AGENAFIBER


Potato-derived insoluble fiber designed for fibre enrichment in bakery and plant-based concepts
AGENAFIBER is an organic potato-derived insoluble fiber designed for fibre enrichment. With very high water-binding-capacity and neutral taste it improves moisture retention, texture and mouthfeel in bakery, confectionery and plant-based meat while supporting clean-label fibre claims.
Key benefits
- Very high water-binding-capacity: increases moisture retention and delays staling in baked goods.
- Texturizing and bulking: improves softness, volume and mouthfeel in low-fat cakes and cookies.
- Structure & stabilisation: reduces syneresis and stabilises particles in batters, fillings and sauces.
- Nutritional & labelling support: high dietary-fibre content enables fibre-claim strategies with modest inclusion levels.
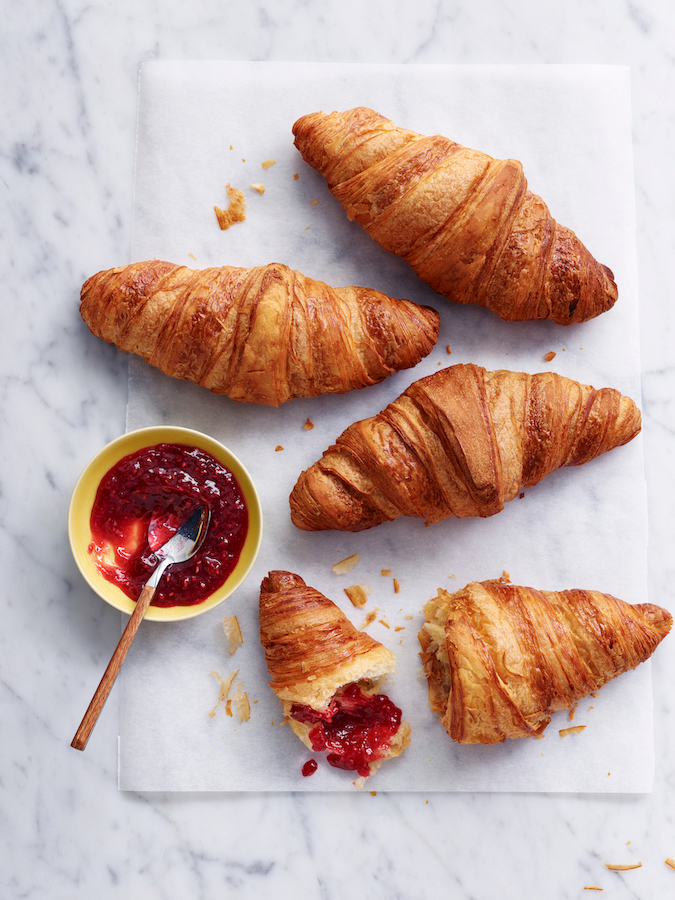
Retains moisture, slows crumb firming and improves slice softness. Use to replace part of flour or fat where softer crumb and extended freshness are required; adjust dough hydration to compensate for water uptake.
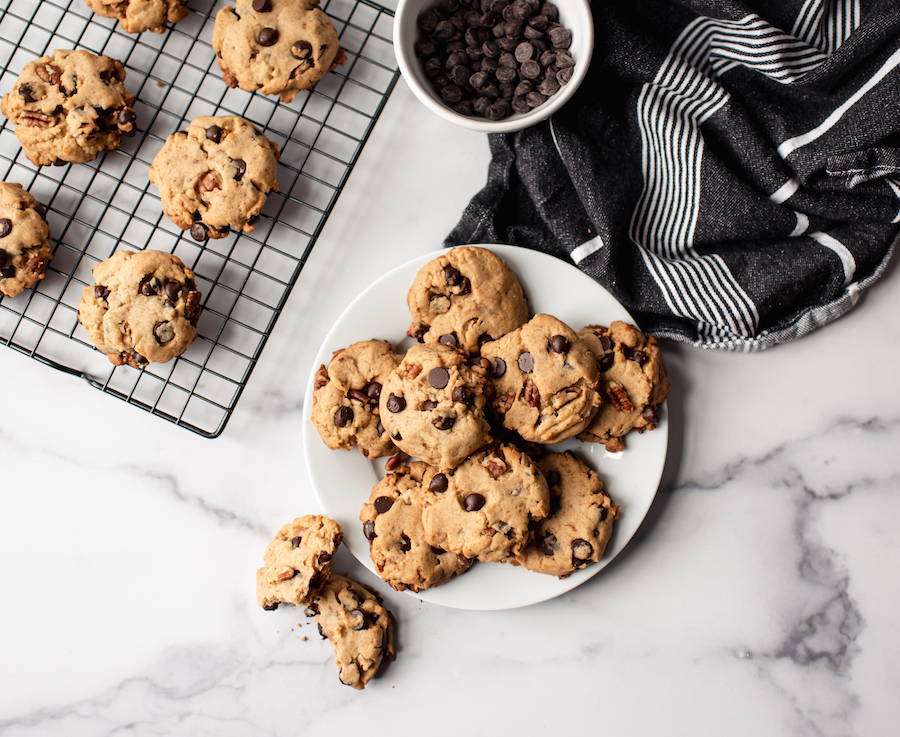
Provides bulking and texture control with neutral flavour. In crisp products, include at low levels or combine with fat-emulsifiers to maintain friability.
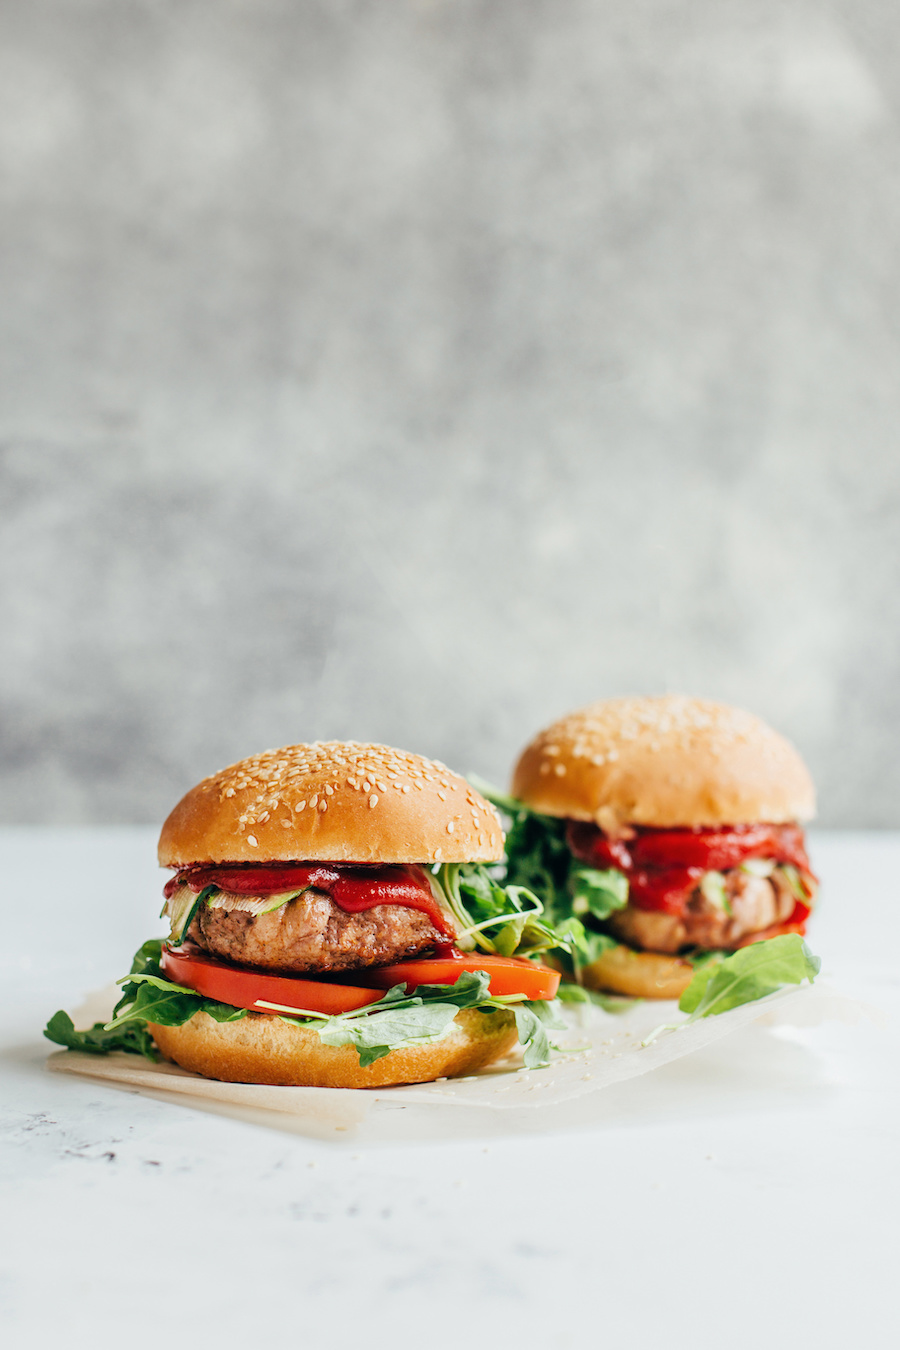
Supports fibrous, meat-like texture when combined with protein systems (e.g., wheat gluten or soy protein); binds water to deliver juiciness and reduce purge. Particle size and hydration profile help create a stable, fibrous matrix.
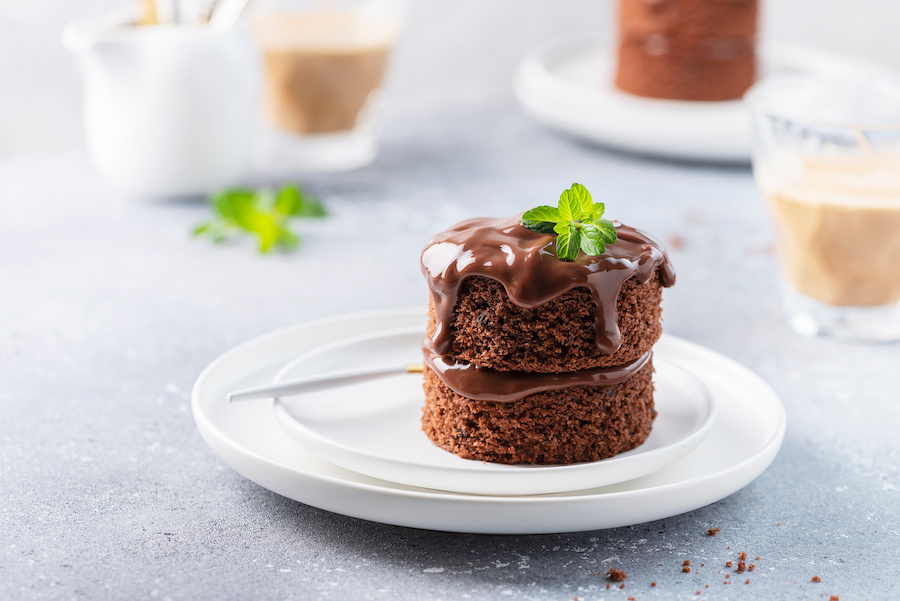
Improves volume and crumb tenderness in low-fat formulations by holding water and contributing bulking without off-flavour; balance sugar/fat levels and mixing to avoid over-tightening the crumb.
Product range
Enhance the activity of your final product by choosing the right variant. We provide formulation guidance, sample trials and scale-up support.
Application concepts
Hydration & addition point: AGENAFIBER hydrates when exposed to water; for even distribution add to the dry mix or pre-blend with flour/other dry ingredients. In high-water systems, consider pre-hydration to avoid lumping.
Mixing & dough handling: Because AGENAFIBER binds water, increase dough water gradually and evaluate dough rheology; more intensive mixing may be required to reach target extensibility. In yeast breads, retained moisture may reduce perceived staling but can influence gas retention — test proofing times.
Compatibility: Performs well with protein networks and starches. For fibrous meat-alternatives combine with binders (gluten, textured vegetable proteins) and control thermo-mechanical processing to create aligned fibres. In emulsions, pair with emulsifiers or proteins to stabilise dispersed phases.
Claim: AGENAFIBER typically contains ≥75 % dietary fibre. To reach a “high in fibre” claim (≥6 g fibre/100 g final product under Codex rules) you need roughly 6 ÷ 0.75 = 8 g AGENAFIBER per 100 g final product (≈8 % inclusion). For a “source of fibre” claim (≥3 g/100 g) the required inclusion is roughly 3 ÷ 0.75 = 4 g /100 g (≈4 %). Use product specification for exact fibre content in formulation calculations.
Formulation insights
From moisture control to fibre claims
AGENAFIBER’s functional effect is driven by high insoluble fibre content and particle morphology. The 19.050 grade exhibits a very high water-binding capacity (≈1 100–2 000 g H₂O / 100 g), whereas 19.051 binds less (≈750–1 500 g / 100 g). Higher WBC increases bound moisture, bulking and viscosity in systems without contributing flavour, which slows staling in bakery and increases juiciness in meat-alternatives.
Average particle size (d50 ≈150–300 µm) moderates hydration speed and mouthfeel: finer fractions hydrate faster and give smoother texture; coarser fractions favour chew and fibrous structure. For emulsions and high-fat systems, combine with suitable emulsifiers or proteins to stabilise phases and avoid fat migration.
Packaging options


We offer a broad range of products and packaging solutions globally. Availability may vary by market due to local requirements. Please contact us to learn more about the options available in your region.