Neutral Alcohol
Neutral Alcohol for Food, Pharma & Industry is a versatile raw material for a broad range of industrial applications where stable solvent performance, process compatibility and consistent supply are essential. AGRANA's neutral alcohol is a renewable, grain-based ethanol with an alcohol content of 96-99.9 vol.%, developed for food, beverages and industrial use. It suits applications such as detergents, cleaning agents, screen wash, adhesives and other technical formulations where ethanol functions as a solvent or carrier. Additionally, it is the main raw material for alcoholic beverages.
Our beverage and food-grade ethanol is a high-purity alcohol used in the production of alcoholic beverages, food ingredients, flavorings and extracts. It meets strict quality and safety standards, ensuring consistency, purity and suitability for human consumption.
Usage of ethanol as solvent in the chemical industry is very common due its excellent solvency, fast evaporation rate, and compatibility with a wide range of substances. This makes ethanol an essential ingredient in many industrial applications. Additionally, it is the key chemical feedstock for the production of ethyl acetate, acetic acid, ethylene, and other industrial chemicals plus it is an important substance of wastewater treatment.
Ethanol is widely used in printing inks as a solvent to dissolve resins, dyes, and pigments, ensuring smooth application and consistent print quality. Its fast evaporation rate supports rapid drying, improved production efficiency, and reduced smudging in flexographic, gravure, and packaging printing processes.
Our ethanol can be ingredient in medicines, disinfectants, sanitizers, and medical formulations. Its antimicrobial properties, high purity, and effectiveness as a solvent make it an essential component in the production of healthcare and pharmaceutical products, including blood treatment and processing.
Ethanol is an essential ingredient in a wide range of cosmetic and personal care products, including fragrances, perfumes, deodorants, skincare, and haircare formulations. It enhances product performance by acting as a solvent, improving ingredient delivery, and providing a refreshing, fast-drying effect.
It is an important ingredient in household and laundry care products as a solvent and cleaning agent. Its effective grease-cutting properties, fast evaporation rate, and ability to enhance the performance of active ingredients make it a valuable component in surface cleaners, detergents, disinfectants, and air care products.
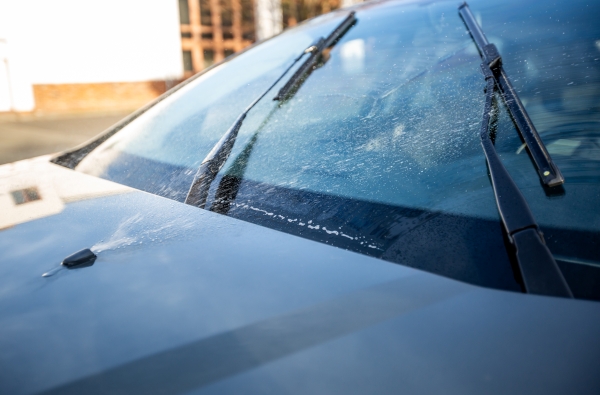
Ethanol is commonly used in winter windshield washer fluids as an antifreeze and cleaning agent. Its low freezing point helps prevent washer systems from freezing in cold temperatures while effectively removing dirt, salt, and road grime from vehicle windshields.
Key benefits
Reliable solvent performance for industrial manufacturers
The right neutral alcohol supports formulation efficiency, application flexibility and stable processing across a broad range of industrial concepts:
- Versatile application range: Suitable for vinegar, beverages, chemical industry, pharma, personal care, detergents, cleaning agents and other technical applications
- Renewable grain-based origin: Produced from feed grain such as wheat and maize, offering a clearly defined and renewable raw material basis for industrial use.
- High alcohol content: Supplied with an alcohol content of 96–99.9 vol.%, supporting consistent solvent and carrier performance.
- Bulk supply efficiency: Available from a minimum order volume of 30,000 liters, AGRANA can supply ethanol by both rail tank cars and road tankers, ensuring flexible and reliable delivery.
Raw materials
Grain-based alcohol for industrial formulation needs
AGRANA's ethanol is produced from feed grain, primarily wheat and maize, and developed for food, pharma & industrial applications.